
How to Brief a Packaging Supplier: Specs That Prevent Costly Mistakes

Most packaging problems do not come from a bad supplier. They come from a brief that left something out.
A skincare brand approves a sample, signs off the price, sends the purchase order, and then production starts revealing gaps. The bottle holds less than the label claims. The pump fits the neck but delivers the wrong dose. The cap threads on but loosens in transit. The print looks right on the proof and wears off in a shipping carton. None of that is exotic. Each one traces back to a field nobody wrote down.
This guide covers what belongs in a packaging brief, why each field exists, and which omissions cost the most. It is written for brands and buyers sourcing bottles, jars, tubes and closures — the point where a vague inquiry turns into quotes you cannot compare and samples you cannot approve.
Key Takeaways
If you only skim one section, this is the short version.
- Overflow capacity is not fill capacity. Fill volume is typically 90–95% of overflow, and internal components such as droppers or pumps eat into it further. Quoting a “30 ml bottle” without saying which number you mean is the most expensive ambiguity in packaging.
- Both halves of the neck code matter. In 24-410, the 24 is diameter and the 410 is thread style. A 24-410 closure will thread onto a 24-400 bottle and still fail to seal.
- Torque is a validated window, not a chart lookup. Published ranges are screening values. The approved range must come from your actual bottle, closure, liner, formula and line, with removal torque measured after a 24-hour dwell.
- Agree your defect classification in writing before production. Without it, “major defect” means one thing to you and another to the factory, and the gap only surfaces in the inspection report: after both sides have committed to the ship date
- Send the identical document to every supplier. Identical inputs are the only way quotations, samples and technical feedback become genuinely comparable.
- Write a change-notification clause. Resin, component, process, decoration, pump and cap changes should reach you before production, not after a reorder looks different.
What a Packaging Brief Actually Is
A brief is not a mood board and not a shopping list. It is a control document that stays alive across quotation, sampling, testing, artwork approval, production, inspection and reorders.
The reason it needs to be one document is that different teams optimise for different things. Sourcing looks at price. Product development looks at appearance. The contract manufacturer looks at filling. The supplier looks at what was quoted. Where those four views are never reconciled in writing, the reconciliation happens later — as rework, delay or a lot you cannot ship.
The standard B2B sequence is worth keeping in view, because each stage consumes the brief: inquiry, specification, quotation, sample, testing, artwork approval, final approval, production, inspection, shipment. A field missing at stage two tends to surface at stage seven or eight, when it is most expensive to fix.
Product and Project Context
Suppliers can only recommend sensibly if they know what the package has to survive. Open the brief with context, not with a part number.
- Product category: serum, toner, cream, cleanser, oil, balm, powder
- Formula type and behaviour: aqueous, gel, emulsion, anhydrous oil, high viscosity, foaming
- Notes that change material choice: pH, alcohol content, essential oil or fragrance load, active concentration, light sensitivity
- Target fill volume and SKU count
- Estimated order quantity and reorder cadence
- Destination market and launch date
- Filling location and whether filling is manual, semi-automatic or automatic
- Whether this is a new launch, reformulation, repeat order or packaging refresh
The filling method line matters more than it looks. Hand filling tolerates loose dimensional variation; an automatic line does not. Stating it up front prevents a supplier from quoting a container that technically matches your spec and jams your equipment.
Capacity: Overflow vs Fill
This is the field most briefs get wrong, and the one with regulatory consequences.
Overflow capacity is the absolute maximum the container holds when filled to the top of the neck with zero headspace. It is an engineering figure. You will never fill to it.
Fill capacity is the usable volume at the correct fill level, leaving room for the closure, thermal expansion and the space that keeps product from spilling when the consumer opens it. It typically lands at 90–95% of overflow.
A bottle marketed as “8 oz” with 240 ml overflow holds roughly 220–228 ml of actual product. If you needed to fill 250 ml, a container specified at 250 ml overflow is already too small — you are looking for something closer to 265–280 ml overflow.
To reach a claim you can defend, start from the overflow figure on the technical drawing and work down:
- Deduct container dimensional tolerance
- Deduct the volume displaced by internal components: pump dip tube, dropper assembly, wiper, rod and applicator, orifice reducer plug
- Deduct required headspace
- Deduct filling equipment tolerance
What remains is your label claim in ml or fl oz. If you are claiming by weight instead, convert using the formula’s specific gravity rather than assuming parity with volume.
In the brief, write both numbers and say which one is the requirement. “Fill volume 30 ml, overflow capacity to be confirmed on drawing” is a usable line. “30 ml” on its own is not. For a broader view of how capacity interacts with format choice, see our guide to cosmetic bottle neck sizes and capacities.
Neck Finish and the Closure System
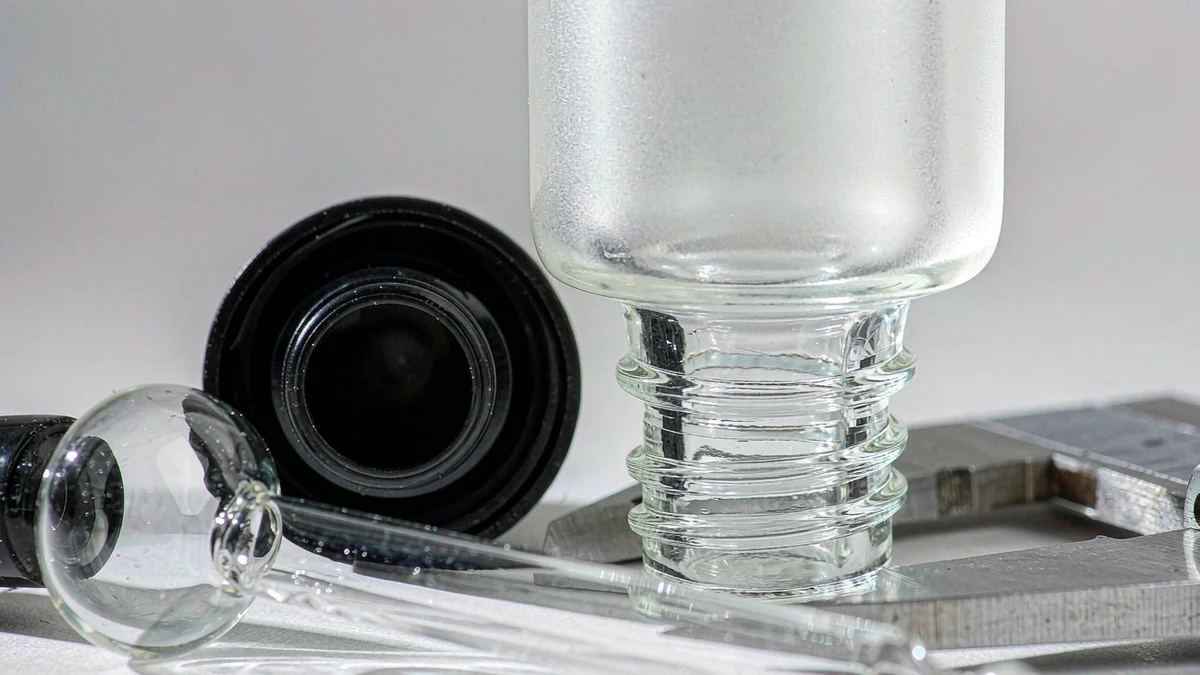
A neck finish is written as two numbers, and both are load-bearing. In 24-410, the 24 is the nominal neck diameter in millimetres and the 410 identifies the thread style. The 400 and 410 series differ in thread height and thread angle, not in outer diameter.
The practical consequence: a 24-410 closure will thread onto a 24-400 bottle far enough to feel secure, while the seal cannot be assumed. Matching only the millimetre figure is the single most common ordering error in this category. Confirm both numbers on the bottle side and the closure side before anything is tooled or ordered.
Other drawing dimensions worth calling out in the brief:
- T: thread diameter
- E: outside neck diameter, which controls whether a tamper-evident band fits without binding
- H: neck height
- Sealing land: the top rim the liner compresses against. Flatness here matters more than most buyers expect, because microscopic imperfections on the sealing surface become leak paths under transport vibration
Then specify the dispensing system as a system, not a part:
- Closure type: screw cap, disc top, flip top, pump, fine mist sprayer, trigger, dropper
- Neck finish match, stated as the full code on both halves
- Pump or sprayer output per stroke, if dosage matters to the product
- Dip tube length, cut angle and whether it must be trimmed to the container
- Liner, gasket or induction seal requirement
- Torque requirement
- Child-resistant or tamper-evident function, if required
- Compatibility with your filling line
- Who assembles the closure: supplier, filler or brand
That last point is a frequent cost surprise. Pre-assembly is labour, and labour is quoted. If you do not say, you may be comparing an assembled quote against a loose-component quote and calling one of them cheap. If you are still deciding between dispensing formats, our comparison of droppers, pumps and airless bottles covers the tradeoffs, and the bottle neck finish guide goes deeper on thread compatibility.
Torque, Liner and Seal Integrity
Torque is where “it fits” and “it seals” separate. Under-tightened, the liner does not contact the finish evenly and the cap loosens in transit. Over-tightened, the closure distorts, skips threads, cracks, or becomes unpleasant to open.
Two measurements matter and they are not interchangeable. Application torque is the force the capper applies. Removal torque is the peak force needed to start opening after the package has settled.
Published tables exist and are useful for framing a trial. Broad screening ranges for continuous-thread closures run roughly as follows:
| Neck finish (mm) | Application torque (in-lb) | Removal torque (in-lb) |
|---|---|---|
| 20 | 8 – 12 | 4 – 6 |
| 24 | 10 – 18 | 4 – 11 |
| 28 | 12 – 21 | 5 – 12 |
| 33 | 15 – 25 | 6 – 15 |
| 38 | 17 – 26 | 7 – 16 |
Treat those as screening values only. Published ranges vary between references, and the approved window has to come from your actual bottle finish, closure resin, liner, formula, filling condition and distribution environment. Two things follow for the brief:
First, ask for the supplier’s recommended range for the specific closure, rather than accepting a generic chart. Second, specify that removal torque is measured after a dwell period, not at the capper. Liners stress-relax, so removal torque decays after application — commonly stabilising somewhere in the region of 40–60% of application torque, with the exact ratio depending on liner family, closure material and temperature. The 24-hour removal torque is the number that tells you about shelf-life seal integrity. The Day-0 reading does not.
Two standards are worth naming in the brief so both sides mean the same thing: ASTM D2063 covers torque-retention measurement for matched container and continuous-thread closure systems over time, and ASTM D3474 covers calibration and use of packaging torque meters. If you are running induction sealing, expect the largest single torque loss there; published research has measured removal-torque drops in the region of 60–72% depending on closure type and container geometry, which is why retorquing exists on those lines.
Liner choice belongs in the same section, matched to formula aggressiveness rather than chosen by default:
- F217 foam / pulp-poly: general purpose, compressible, resealable
- Induction foil: hermetic and tamper-evident
- PTFE-faced or high-barrier foil: solvent, ester and aggressive fragrance systems, where standard liners can swell or degrade
- EPE foam: low cost with decent recovery, but more compression set under heat
- TPE / elastomer: better rebound; confirm food-contact compliance and ageing behaviour
Pressure-sensitive liners are generally unsuitable for liquids. And one geometry check that catches real failures: the closure must seat on the land area without bottoming out on the shoulder, otherwise the liner never compresses at all.
Material, Gram Weight and Structure
Material is usually the first field brands fill in and the one they under-specify. Record the preferred resin or glass type, an acceptable alternative if you have one, and the appearance route — clear, translucent, frosted or opaque. If recycled content is in scope, state the target PCR percentage and, just as importantly, the expected colour range and how sample approval will handle batch variation.
Then add the fields buyers most often skip:
- Gram weight: the empty container weight. It drives resin cost and freight cost, and it appears on every spec sheet for a reason
- Wall thickness expectation, where it matters to feel or performance
- Top-load requirement: the vertical force the container must survive during capping and warehouse stacking
- Base shape and stability
- Label panel dimensions and any contour that limits usable decoration area
- Filling temperature, if the product is not filled cold
Lighter is not automatically better. Aggressive lightweighting can push a container below its top-load requirement, and uneven wall distribution creates weak points even when total weight looks acceptable — especially on tall, narrow or heavily contoured designs. If you are specifying PCR, note that recycled resin sometimes needs slightly higher gram weight to reach the same structural performance. That is an engineering consequence, not a quality defect.
Material choice also interacts with the formula in ways a drawing cannot show. Paneling, migration, stress cracking and fragrance scalping tend to appear over weeks, not in a two-day trial. Our guide to packaging compatibility testing covers how to structure that work before bulk production.
Decoration and Artwork
Decoration is where briefs get poetic and quotes get incomparable. “Premium matte with gold logo” is a direction, not a specification.
Specify instead:
- Print method and colour count: the two together, since method drives tooling and colour count drives cost per pass
- Pantone or approved colour standard, plus how colour will be judged
- Hot stamp, emboss or deboss zones with position and size
- Matte or gloss varnish zones, where partial finishes are intended
- Label route: pressure-sensitive, shrink sleeve, in-mould
- Artwork status: final, in progress, or supplier to advise dielines
- Cap material and finish, and whether it matches or contrasts the body
Two decoration failure modes are worth naming explicitly in the brief, because they have different fixes. Adhesion failure is decoration peeling or wearing without any product contact. Compatibility failure is chemical interaction between the formula and the decoration degrading appearance or function. Remedies differ: curing properties and dwell time, ink or lacquer chemistry, alternative foils, or a UV-cured clear topcoat that isolates the decoration from the formula. Ask for decorated components to be tested for both, with your actual formula rather than a stand-in.
Colour judgement needs a stated condition too. Visual evaluation should use a standardised light source — D65, around 6500 K, is the common reference. Approving a finish in a dark warehouse or under mismatched lighting is how colour-variance disputes start. For a fuller comparison of methods and their cost profiles, see our overview of cosmetic packaging decoration options.
Quality Standard: Defect Classification and AQL
This is the section most brands leave out entirely, and it is the one that decides who pays when a lot is disputed.
Inspection of packaging components normally follows ISO 2859-1, sampling inspection by attributes. It defines how many pieces to draw from a lot and the accept/reject numbers that follow. Two things need to be in the brief.
Inspection level. ISO 2859-1 defines general inspection levels GI, GII and GIII. GII is the standard default for ongoing production with an established track record. GIII draws a larger, more discriminating sample and is the sensible choice for a first order with a new supplier, after a prior quality incident, or where a failure discovered at destination would be expensive. GI minimises inspection cost at the price of discrimination and is not a good fit for a first run.
AQL by defect class. Common practice assigns zero acceptance to critical defects, roughly 1.5–2.5 to major, and 4.0–6.5 to minor. Tighter numbers suit higher retail positioning. AQL 6.5 is generally too lenient for commercial packaging. Put the actual numbers in the supplier quality agreement rather than leaving them implied.
To make that concrete, here is what a GII single-sampling plan looks like under normal inspection:
| Lot size | GII sample size | AQL 2.5 major, accept / reject | AQL 4.0 minor, accept / reject |
|---|---|---|---|
| 1,201 – 3,200 | 125 | ≤7 / ≥8 | ≤10 / ≥11 |
| 3,201 – 10,000 | 200 | ≤10 / ≥11 | ≤14 / ≥15 |
| 10,001 – 35,000 | 315 | ≤14 / ≥15 | ≤21 / ≥22 |
The numbers only work if both parties agree what counts as a defect, and at what severity. Write the classification table into the brief. A workable starting point for cosmetic containers:
- Critical: foreign matter or glass shards inside the container, cracks penetrating the wall, sharp flash or burrs on closure rims, contamination, missing country of origin or prohibited regulatory text. Zero acceptance
- Major: leakage, stripped or deformed threads that prevent secure torque, seized pump, dimensions or fill capacity outside tolerance, closure non-conformance, print typos or misregistration on the primary display face, coating delamination or widespread paint peeling
- Minor: fine scratches on secondary surfaces, micro-bubbles, isolated dust, slight colour variance within an approved limit sample
Severity also depends on where the defect sits. Visual zoning is standard practice and worth stating: Zone A is the primary consumer-facing area — front logo and print, cap top, tube display face — and is weighted hardest. Zone B covers sides and back where ingredients and barcodes live, tolerating micro-imperfections unless legibility or the barcode is affected. Zone C covers the base, internal threads, pump interior and master carton, where cosmetic defects are minor provided function is unaffected.
Finally, name the documentation you expect. Buyers commonly request ISO 9001 for quality management and ISO 22716, the GMP standard for cosmetics. Depending on market, REACH documentation, food-contact statements, or an EU Declaration of Compliance chain covering liner, fitment, coating and inks may apply. Ask for copies and verify them rather than accepting a logo on a website.
Commercial Terms, Logistics and Change Control
The commercial block is usually present but thin. Complete it:
- MOQ per component and per decoration route: decoration frequently carries its own minimum, separate from the container
- Sample cost and sample lead time
- Tooling or mould cost, and whether it is quoted separately or amortised into unit price
- Unit price at your realistic quantity bands, not an aspirational one
- Production lead time and artwork proofing turnaround
- Payment terms and shipping terms
MOQ deserves a note. Stock components and custom tooling behave very differently, and a single MOQ figure across a mixed spec is usually a sign the question was not asked properly. Our explainer on cosmetic packaging MOQ covers why the number moves.
Logistics fields are cheap to write and expensive to omit:
- Inner packaging method
- Carton dimensions and pieces per carton
- Gross weight per carton
- Loading quantity per container
- Shipping method and destination port or door
Then add the clause most briefs never include. Specify that the supplier notifies you before changing raw material, component, production process, decoration, pump or cap. For a brand reordering the same packaging over several years, this single sentence prevents the slow drift where year three does not match year one. Pair it with a retained golden sample — the physically approved reference that future production is measured against, alongside the written spec.
The Five Omissions That Cost the Most
If the full brief feels like a lot, these five carry disproportionate weight:
- Capacity stated without saying overflow or fill. Leads to underfill, label-claim exposure and sometimes a container that cannot hold the product it was bought for
- Neck finish quoted by diameter only. Produces closures that thread on and do not seal
- No torque specification or validation plan. Produces transit leakage or a cap the consumer cannot open
- No agreed defect classification and AQL. Turns every quality question into a negotiation with no reference point
- No change-notification clause. Turns a successful first order into an inconsistent reorder
None of these need engineering resource to fix. They need a document, filled in once, sent identically to every supplier you are asking to quote.
Ready to Brief Your Next Packaging Project?
Send us your fill volume, formula type, neck finish, decoration direction and target quantity, and our team will come back with a spec-level quotation you can compare line by line.
FAQ
What is the minimum information a packaging supplier needs to quote?
Product type, formula notes, fill volume, container format, closure or dispenser route, decoration direction, artwork status, target quantity, destination market and required date. That set is enough for a supplier to return a realistic quotation. If you do not know the technical specifications yet, send product photos, reference packaging and target market instead, and ask the supplier to propose options.
Why do quotes from different suppliers vary so much?
Usually because each supplier filled in your gaps differently. Where a brief omits gram weight, liner type, colour count or assembly responsibility, suppliers substitute their own assumptions and quote different products. The fix is not more negotiation, it is an identical specification document sent to everyone.
Is overflow capacity or fill capacity the number I should put on the label?
Neither directly. Start from overflow capacity on the technical drawing, deduct container tolerance, the volume displaced by internal components such as a dropper or pump, required headspace and filling equipment tolerance. What remains is your defensible label claim. If claiming by weight, convert using the product’s specific gravity.
Can I just take torque values from a published chart?
Use a chart to frame a trial, not to release production. Published ranges vary between references and do not know your liner, formula or filling line. Ask the closure supplier for their recommended range, then validate on the actual package and record removal torque after a 24-hour dwell rather than at the capper.
What AQL level should I ask for on a first order?
General inspection level GIII is the common choice for a first order with a new supplier, because it draws a larger, more discriminating sample than the GII default. Typical AQL assignment is zero acceptance for critical defects, 1.5–2.5 for major and 4.0 for minor, tightened for higher retail positioning. Whatever you choose, put the numbers and the defect classification table into the supplier agreement before production starts.